 HWAMDA

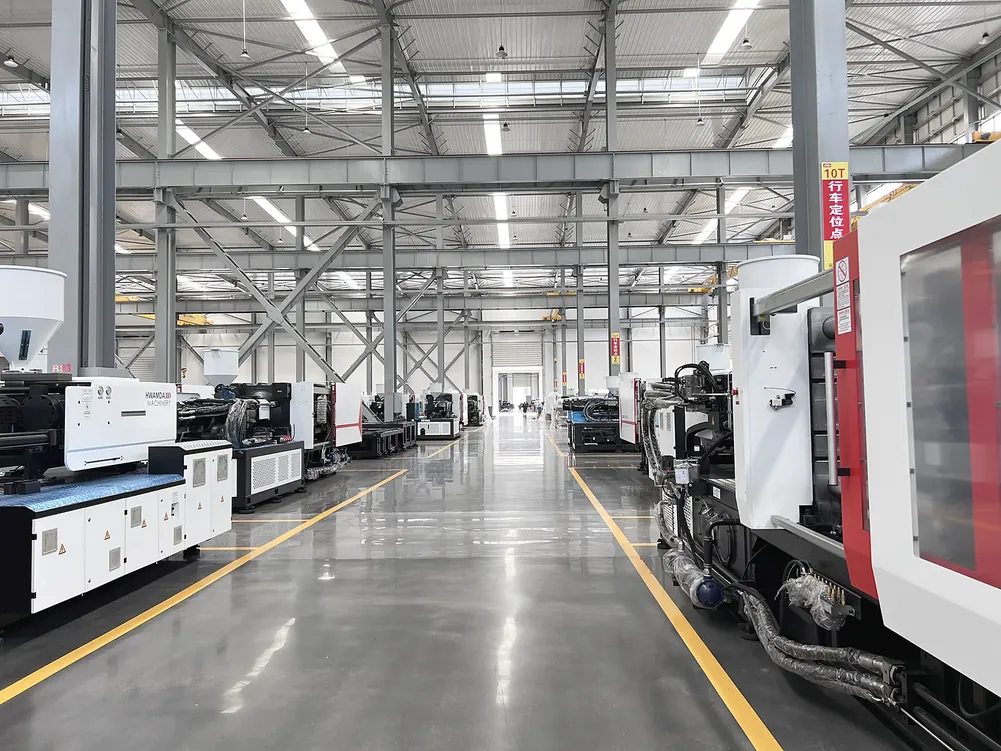
What a turnkey injection molding line includes
A turnkey line is a complete production cell planned around one product: the injection molding machine, the mold, material handling, cooling, part removal and the plant utilities that tie them together. Instead of buying each item separately and solving the interfaces on the shop floor, the buyer receives one configuration in which clamping force, shot size, mold dimensions, robot reach, chiller capacity and conveying rate have been matched to each other before anything is built.
HWAMDA coordinates turnkey projects from the first part review through installation, commissioning and operator training. The goal is simple: a line that arrives with its scope confirmed, is tried against agreed acceptance requirements before shipment, and reaches production in your plant with a clear plan.
- Injection molding machine
- Selected from the M8SII, SP6, PET preform, DU II two-platen, FCII or DP series according to part weight, mold size, cycle target and material.
- Mold
- Cavity count, runner system, cooling layout and ejection matched to the machine platens, tie-bar spacing, opening stroke and injection capacity.
- Auxiliary equipment
- Resin dryers, hopper or vacuum loaders, central conveying, chillers, mold temperature controllers and granulators sized to the real throughput of the cell.
- Robot and automation
- Sprue pickers, three-axis or servo take-out robots, IML label handling, stacking, counting and conveyors, defined by how finished parts must leave the cell.
- Conveying and packing
- Belt conveyors, part stacking and packing points arranged so that the operator workload matches the cycle time.
- Utilities planning
- Power, cooling water, compressed air, floor loading and crane access specified early so the building is ready when the equipment arrives.
Project phases from requirement review to production support
Every turnkey project follows the same sequence. Clear deliverables at each phase keep decisions moving and make it obvious which inputs are still needed.
| Phase | What happens | Typical output |
|---|---|---|
| 1. Requirement review | Part drawings or samples, material grade, target output, decoration method and plant conditions are collected and reviewed. | Confirmed product and production targets |
| 2. Configuration and layout | Machine model, injection unit, mold concept, automation and auxiliaries are matched; the cell layout and utilities list are drafted. | Configuration proposal and layout drawing |
| 3. Mold and machine build | Mold design is approved, machine and auxiliaries are built to the agreed configuration and interfaces. | Approved mold design, build schedule |
| 4. Factory trial and acceptance | The machine and mold run together at the factory; sample parts and process settings are checked against the agreed acceptance requirements. | Trial samples, trial report, acceptance record |
| 5. Shipping | Equipment is cleaned, protected, packed and documented for export; spare parts and manuals travel with the shipment. | Packing list, shipping documents |
| 6. Installation and commissioning | Equipment is positioned, leveled and connected to utilities; the line is commissioned and production parameters are established. | Commissioning record |
| 7. Training | Operators and maintenance staff are trained on machine operation, mold changes, auxiliaries and routine maintenance. | Trained team, maintenance plan |
| 8. Production support | Remote technical support, spare parts supply and maintenance guidance continue after start-up. | Ongoing support channel |
What the customer provides
The fastest projects start with good product data. Missing values are normal at the beginning; the requirement review identifies what is still needed before a configuration is proposed.
- Product definition
- 3D model or 2D drawing, or physical samples, with target part weight, wall thickness and critical dimensions.
- Material
- Resin type and supplier grade, melt flow index, colorant or masterbatch ratio and any regrind percentage.
- Output target
- Required pieces per hour or per year, working shifts and the acceptable cycle time range.
- Decoration and handling
- Printing, IML, stacking, counting or packing requirements for the finished part.
- Plant information
- Available floor area, building height, crane capacity, voltage and frequency, cooling water and compressed air supply.
- Acceptance criteria
- The dimensions, weights, visual standards and cycle checks that define a successful factory trial.
Plant utilities checklist
Utilities are the most common cause of delay at installation. The values below are typical planning ranges for a medium-size injection cell; the configuration proposal gives the exact figures for your line.
| Utility | What to plan | Typical planning values |
|---|---|---|
| Electrical power | Supply voltage and frequency, total connected load of machine, heaters and auxiliaries, cable and breaker sizing. | 380–415 V / 50 Hz or 440–480 V / 60 Hz three-phase; plan the full cell load, not only the machine motor |
| Cooling water | Chiller capacity for the mold, tower or plant water for the hydraulic oil cooler, pipe sizes and water quality. | Mold water often 10–15 °C from a chiller; oil cooler water 25–32 °C; filtered, treated water |
| Compressed air | Pressure and flow for robots, IML, air ejection, vacuum loaders and blowers. | 0.6–0.8 MPa dry, filtered air; IML and blow-off cells use noticeably more flow |
| Floor and foundation | Floor loading under the machine, leveling, anchoring and space for mold changes and maintenance. | Level concrete floor rated for the machine weight plus mold; clearance around the cell for service |
| Crane and access | Crane capacity for the heaviest mold half, door size and route for delivery. | Crane rated above the full mold weight with a margin; check door height for the machine and robot |
Confirm local electrical standards and water quality requirements with your facility engineer before installation.
Example turnkey cells
The examples below show how the same planning approach applies to different products. Each is configured for the specific part, mold and output target of the project.
- Thin-wall cup line
- An SP6 high-speed machine with a multi-cavity cup mold, take-out robot with stacking and counting, chiller and mold temperature control, and vacuum loading. Fast injection and short cooling make chiller and stacking capacity as important as the machine itself.
- PET preform line
- A PET preform machine with a 25:1 PET screw, a 16–96 cavity hot runner preform mold, dehumidifying dryer, chiller with low-temperature mold water, and post-mold cooling and conveying. Resin drying is planned as part of the cell, not as an afterthought.
- Paint bucket IML cell
- An M8SII paint bucket machine with a bucket mold, IML robot with label magazine and mandrel, lid production planning and stacking conveyor. The robot, mold and label format are defined together.
- Crate line
- An FCII crate machine with a large crate mold, robot or conveyor take-out, chiller, mold temperature controller and granulator for runners and rejects. Mold weight and crane capacity are checked early.
How to start a turnkey project
Send the product drawing or samples, the resin grade, the target output and a short description of your plant. If you already own a mold, add its dimensions, weight and photos. From this information a sales engineer prepares the first configuration and identifies any inputs still missing.
Useful planning tools include the tonnage calculator and the shot size calculator in the resources section. When you are ready, use the request a quote form and mention that you need a complete line.
FAQ
Frequently asked questions
What is included in a turnkey injection molding line?
The machine, mold, auxiliaries such as dryers, loaders, chillers and mold temperature controllers, robot and conveying, plus utilities planning, factory trial, installation, commissioning and training. The exact scope is confirmed in the configuration proposal.
Can I use my existing mold in a turnkey line?
Yes. Send the mold drawing, dimensions, weight, cavity count and sample parts so the machine, automation and auxiliaries can be matched to it.
How is the line accepted before shipment?
The machine and mold run together in a factory trial, and sample parts and process settings are checked against the acceptance requirements agreed in the contract. You can attend the trial or review the trial report and samples.
Which utilities must my plant prepare?
Three-phase power for the full cell load, cooling water for the mold and hydraulic oil cooler, dry compressed air, a level floor rated for the equipment and a crane sized for the mold. The configuration proposal lists the exact values.
Do you provide training for operators?
Yes. Operator and maintenance training is part of commissioning and covers machine operation, mold changes, auxiliaries and routine maintenance.
What information do you need for a first proposal?
A part drawing or sample, the resin grade, target output, decoration method and basic plant data. Unknown values can be clarified during the requirement review.