 HWAMDA
Preform
Weight, neck finish, drawing, resin and accepted quality criteria.
Tell us your preform weight and cavity count, and we match the HMD-PET model, injection unit and mold interface. Six models from 2,180 to 6,000 kN.
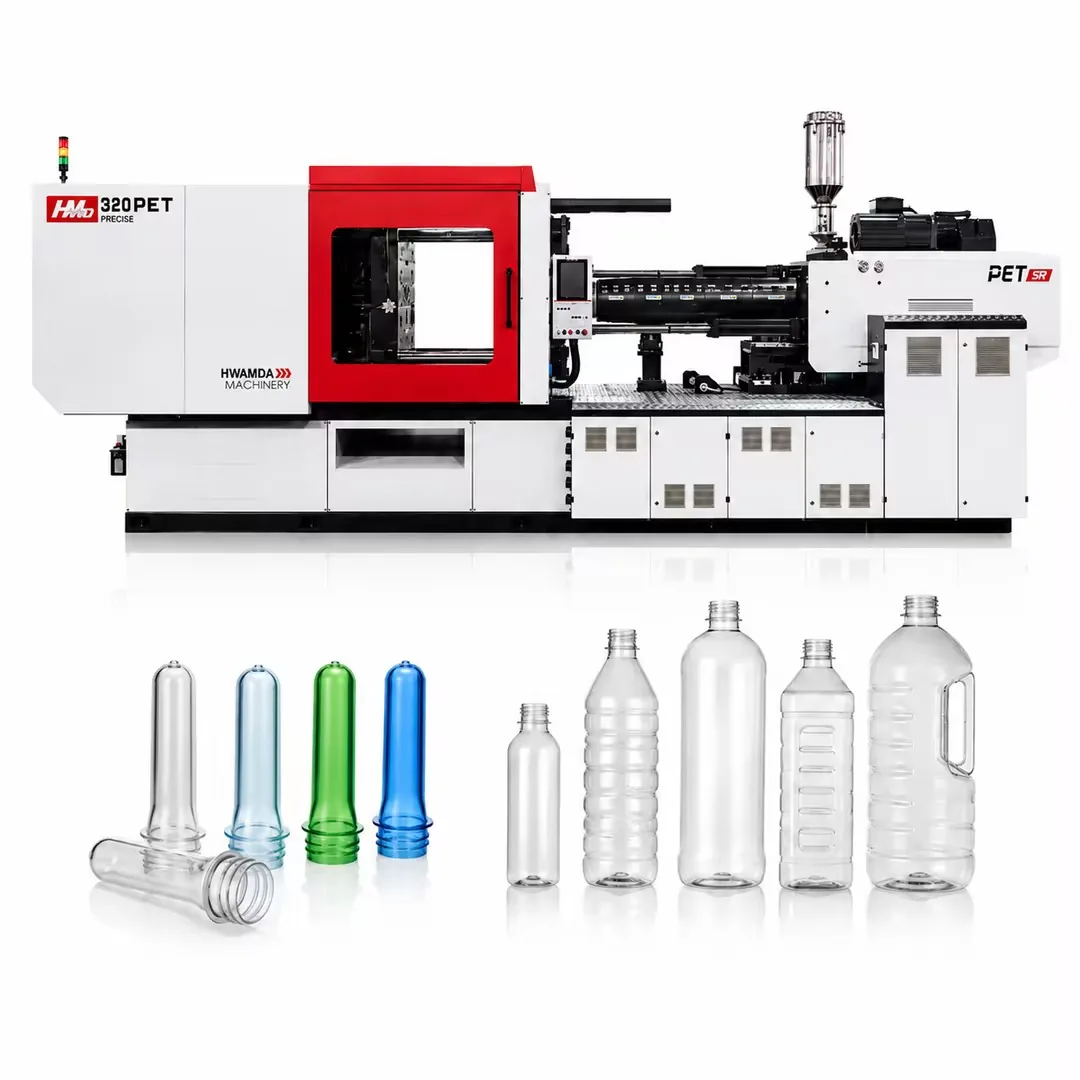
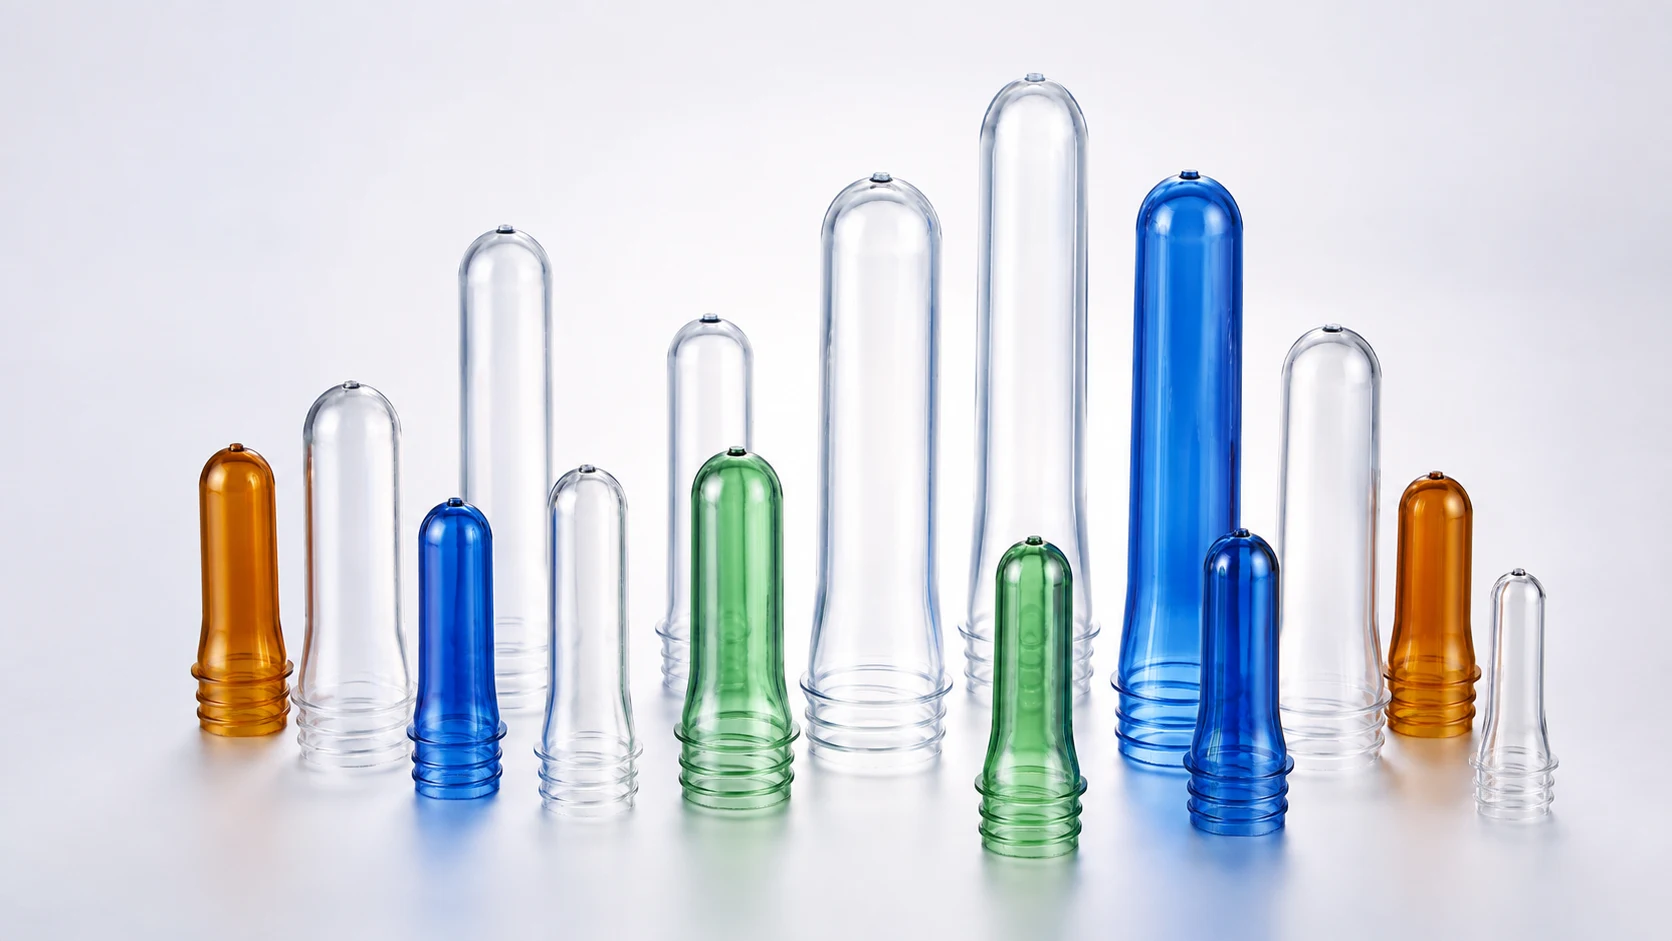
This PET bottle preform machine range covers 28 mm and other neck finishes for water, carbonated drinks, edible oil, wide-mouth jars and large-format containers. Final selection depends on preform weight, cavity count and target output.
Start with the preform and required output—not tonnage alone. HWAMDA checks the complete project data before recommending the machine and injection-unit configuration.
Weight, neck finish, drawing, resin and accepted quality criteria.
Cavity count, dimensions, hot runner, cooling and machine interfaces.
Target cycle, pieces per hour, take-out and downstream handling.
Voltage, drying, cooling water, compressed air and plant layout.
Compare six PET preform molding machine sizes from 2,180 to 6,000 kN, then match the injection unit to preform weight, cavity count and required output.
Recorded on HMD-PET machines during customer mold trials before shipment. Actual results depend on preform design, mold and cooling.
Preforms per hour = cavities × 3,600 ÷ cycle time in seconds, before downtime and rejects.
HWAMDA PET preform machines have been delivered to customers in Kenya, Kazakhstan, Nigeria, Brazil and more.
Send your preform weight and cavity countEach PET preform injection machine is based on the M8SII platform and configured for water, carbonated-beverage, edible-oil, wide-mouth and large-format preforms.
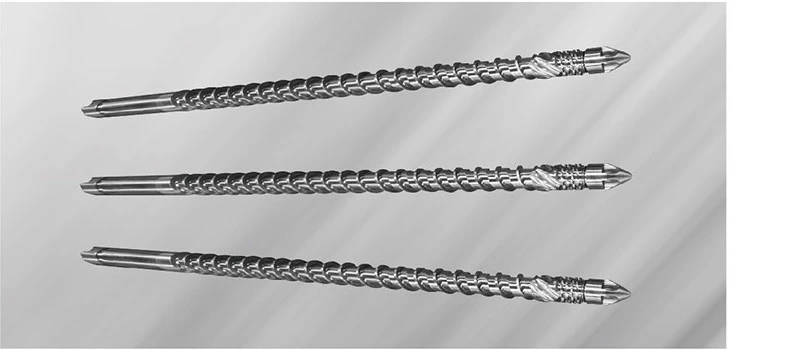
A dedicated screw ratio supports PET plasticizing and preform transparency.
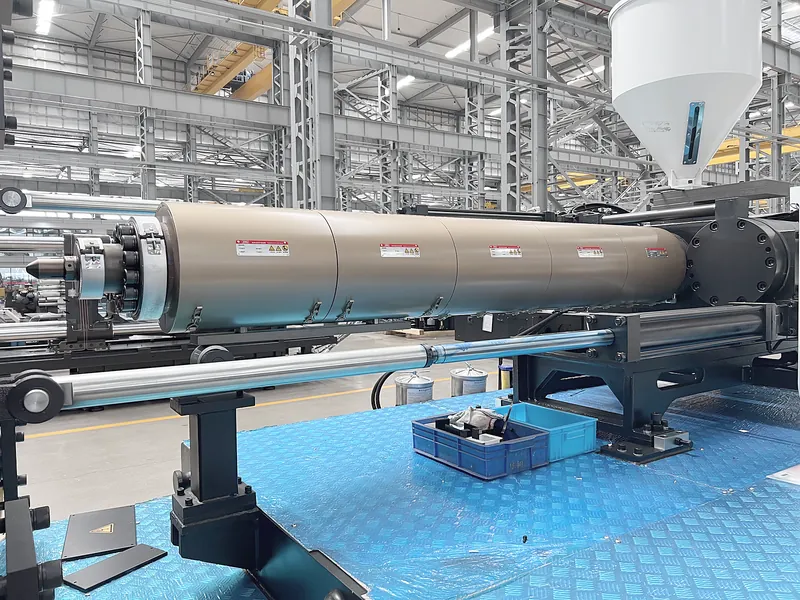
Linear guides balance movement and improve injection stability.
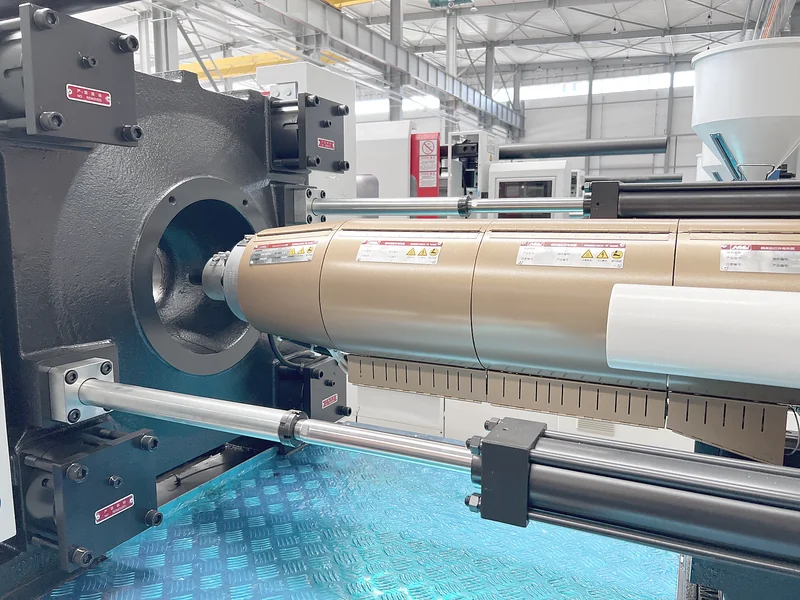
Twin injection cylinders reduce return resistance during high-pressure injection.
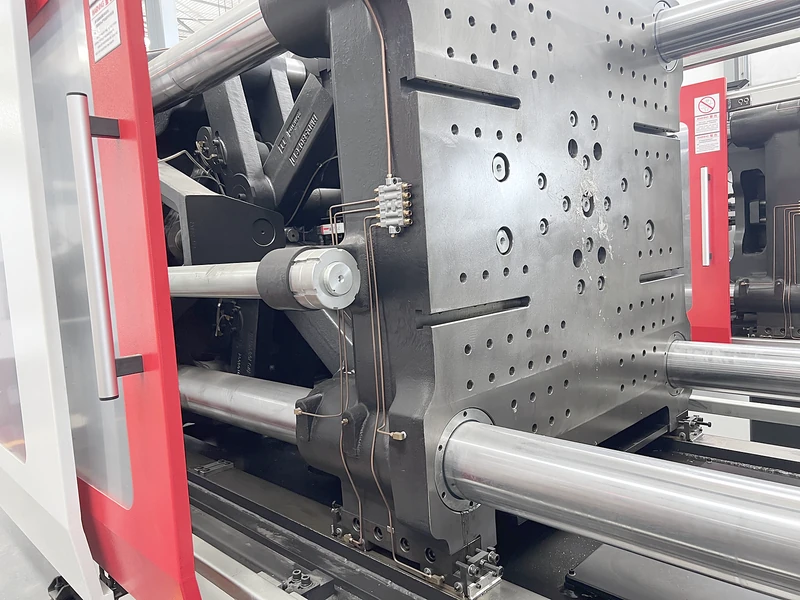
The clamping structure is designed for stable movement and broad mold accommodation.
Longer stroke and higher ejector force support long and multi-cavity preform molds.
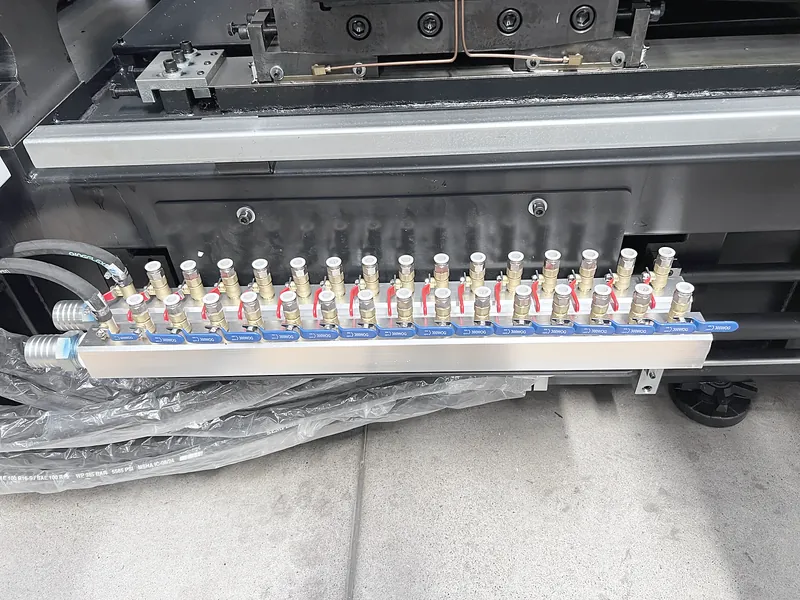
Quantitative lubrication and fixed-point delivery reduce oil loss and support reliability.
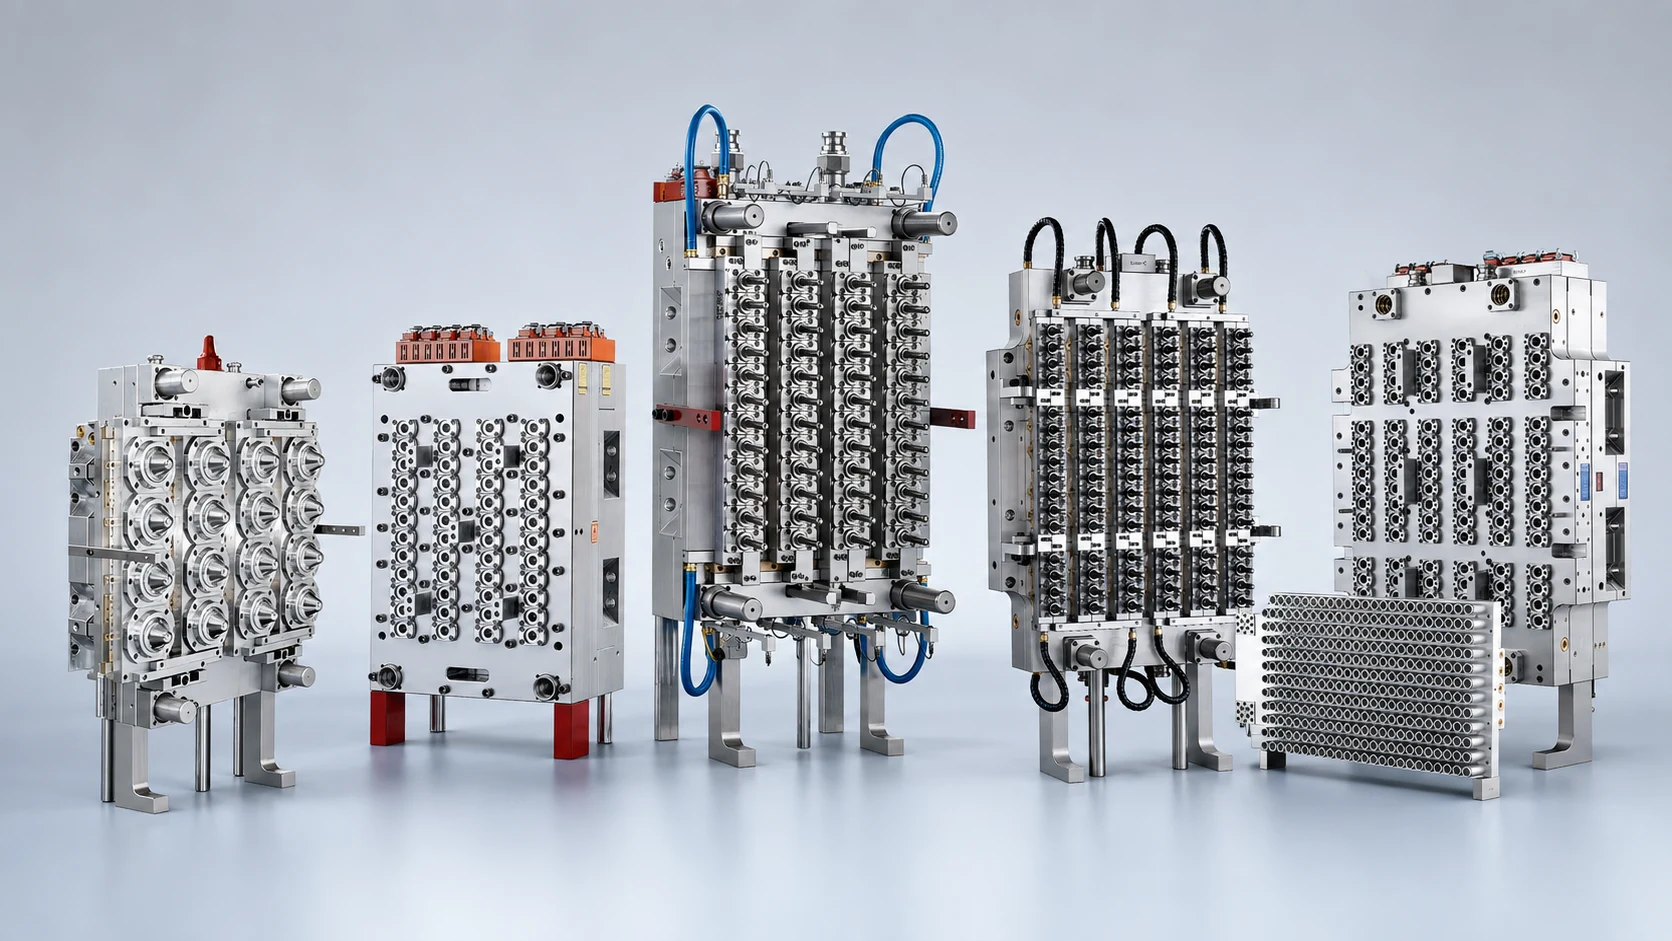
The machine range can be configured for 16-, 24-, 32-, 48-, 64-, 72- and 96-cavity preform molds, plus 28 mm neck, wide-mouth and large-format projects. Final model compatibility depends on more than clamping force.
There is no single cycle time for every PET project. Stable hourly output is estimated from the confirmed preform, mold, cooling system, machine recovery and handling sequence.
More cavities can increase hourly output, but also change shot size, mold size, cooling demand and investment.
Heavier preforms require more injection capacity, plasticizing capacity and cooling time.
Mold design, chilled-water temperature and flow strongly influence the stable cycle.
Robot motion and downstream transfer must keep pace without damaging hot preforms.
Preforms per hour = cavities × 3,600 ÷ cycle time in seconds, before downtime and rejects.
Example from the reference table: HMD430PET with a 72-cavity mold at a 9.9 s cycle gives 72 × 3,600 ÷ 9.9 ≈ 26,180 preforms per hour. Apply your own uptime and reject rate to plan daily output.
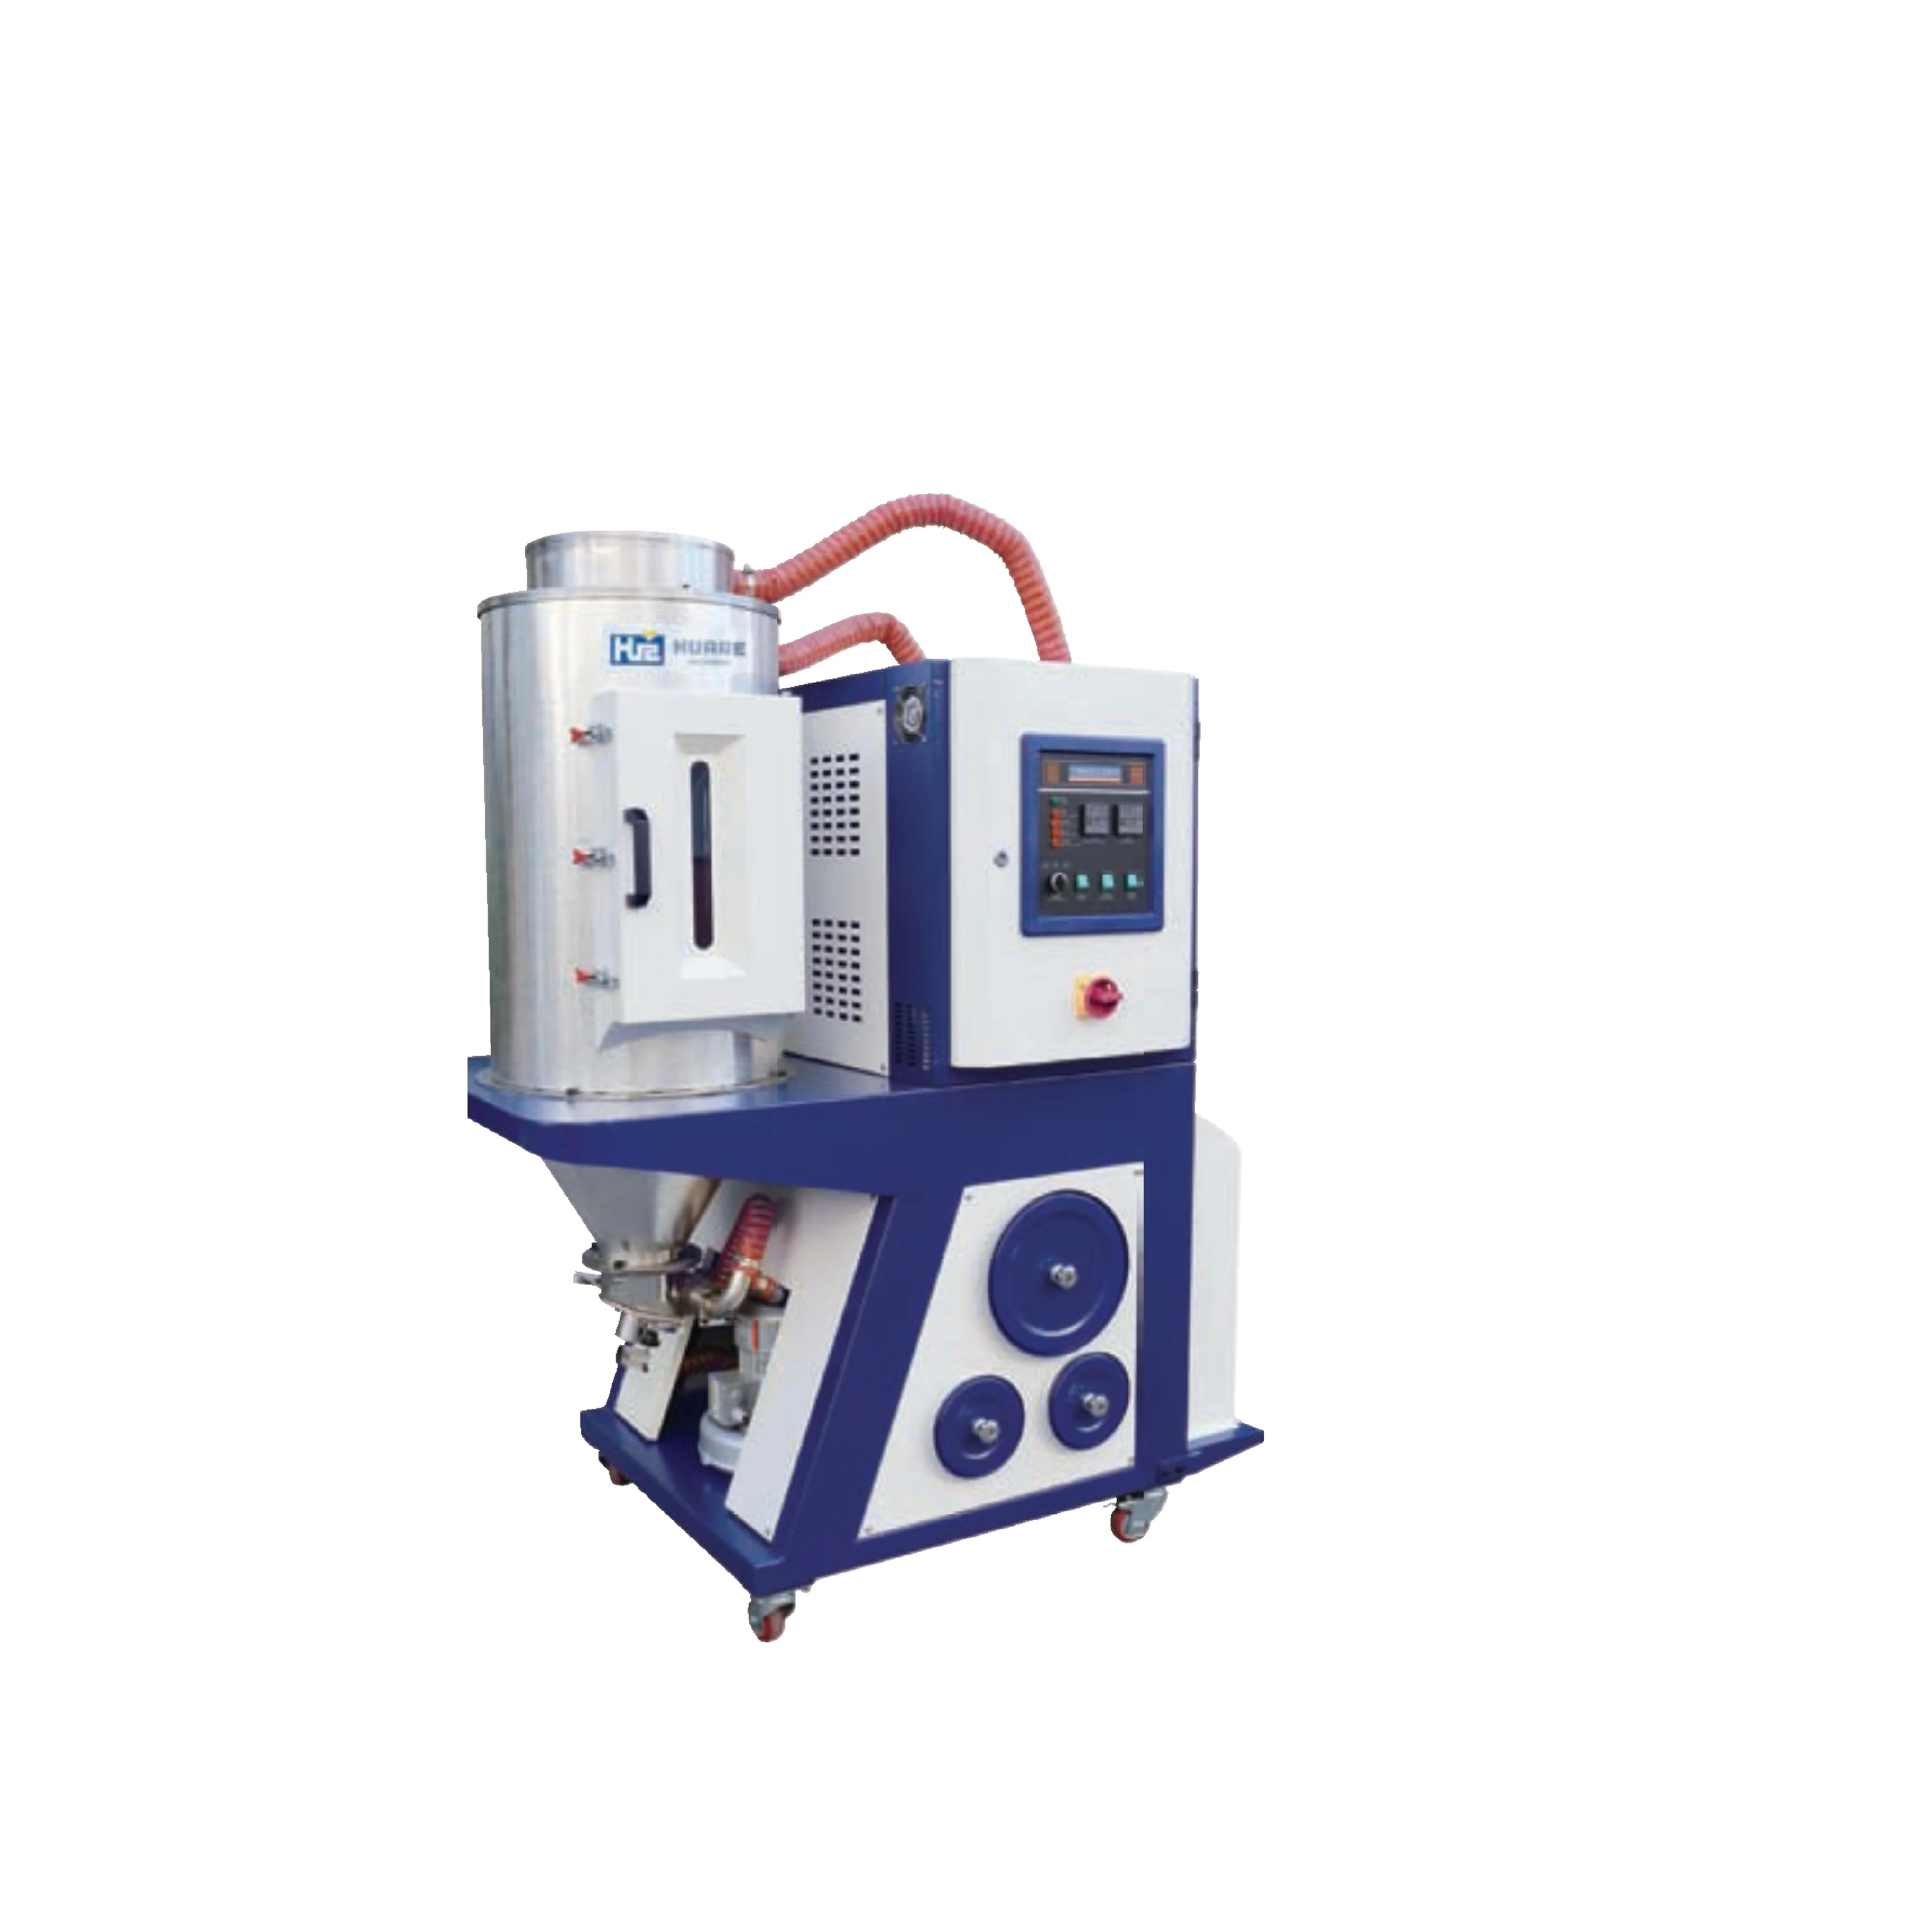
PET absorbs moisture from the air. The resin must be dehumidified, dried and conveyed under controlled conditions before it reaches the screw. Final settings must follow the resin supplier data and verified production conditions.
Auxiliary equipment is sized as part of the production cell. The final list depends on resin consumption, mold cooling demand, color dosing, compressed air, take-out and site conditions.
A three-in-one dehumidifying, drying and loading system prepares PET before plasticizing.
The industrial water chiller is matched to mold circuits, water temperature, flow and heat load.
Plant air supports the specified machine, valve and automation requirements.
Masterbatch dosing and robot handling are selected around color control and the production layout.
Drying, mold cooling, compressed air, take-out, output planning and site requirements for the whole preform line are covered on the production line page.
These are selectable catalogue items. The quotation should include only the functions required by the confirmed mold and process.
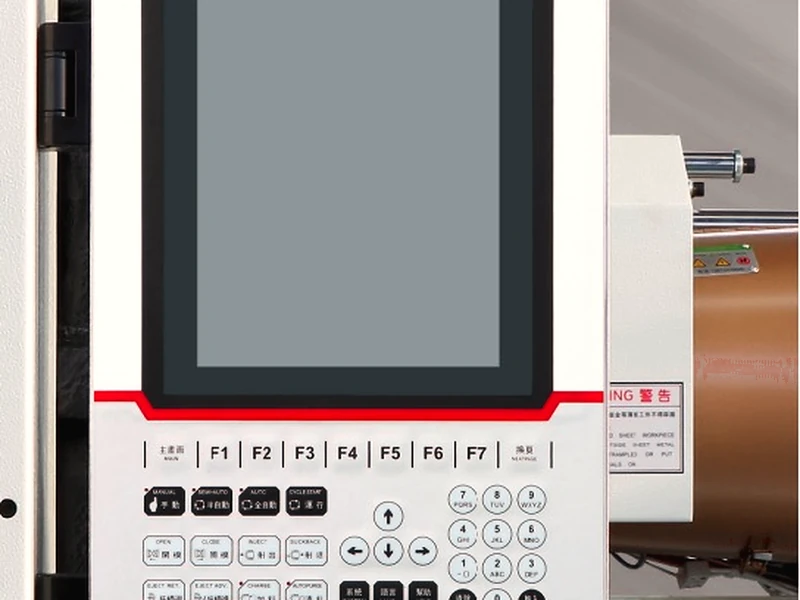
Fully enclosed clamping-area cover with mold dehumidifier.
Built-in cooling-water piping for a cleaner installation.
Photo-sensor confirmation helps protect the mold before the next cycle.
Selectable needle-valve modes with adjustable timing.
Reserved signals for conveying, packaging count and alarms.
Optional plasticizing and ejection synchronization for shorter cycles.
Price depends on the selected machine and injection unit, preform weight, mold cavity count, auxiliaries, automation, utilities, logistics and service scope. Every quotation is prepared for your project.
Model size, screw diameter, shot requirement and plasticizing demand define the base configuration.
Cavity count, mold dimensions, hot runner, cooling and ejection affect the integration scope.
Drying, loading, dosing, cooling, compressed air and robot requirements are quoted as needed.
Destination, voltage, installation, trial, training, logistics and acceptance scope affect the final quotation.
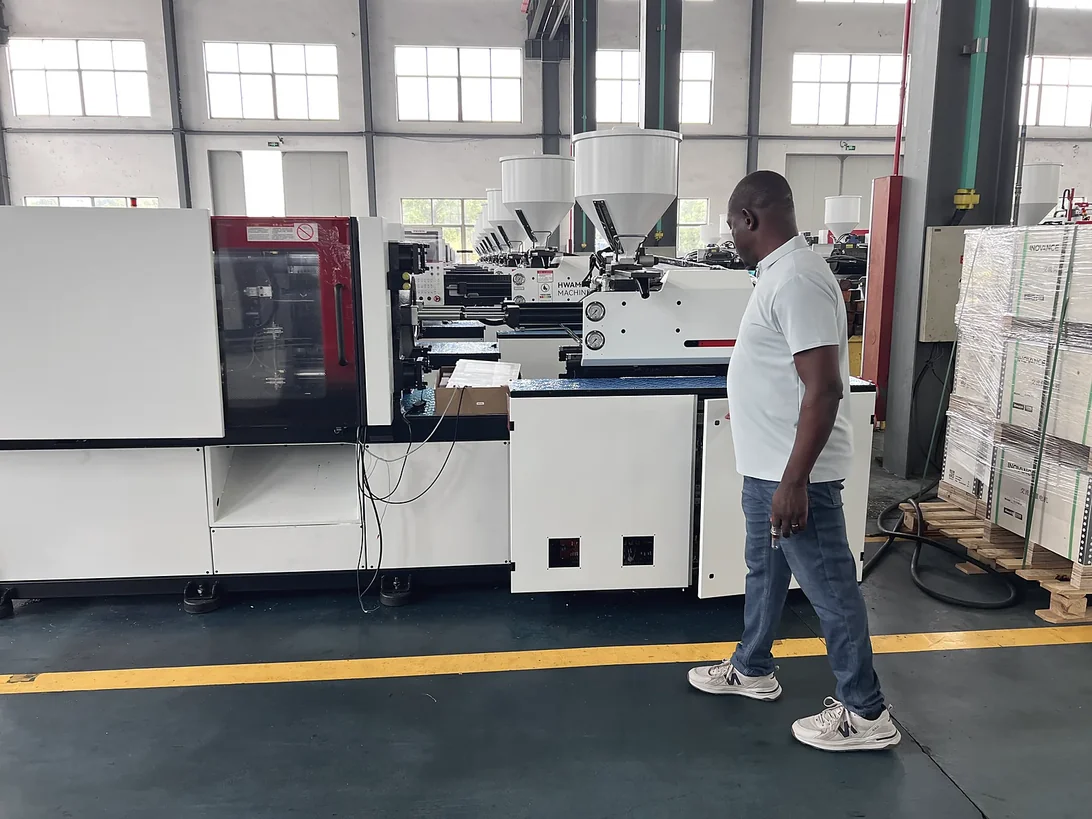
Trial records and inspection images help buyers evaluate appearance, part weight and critical dimensions before shipment.
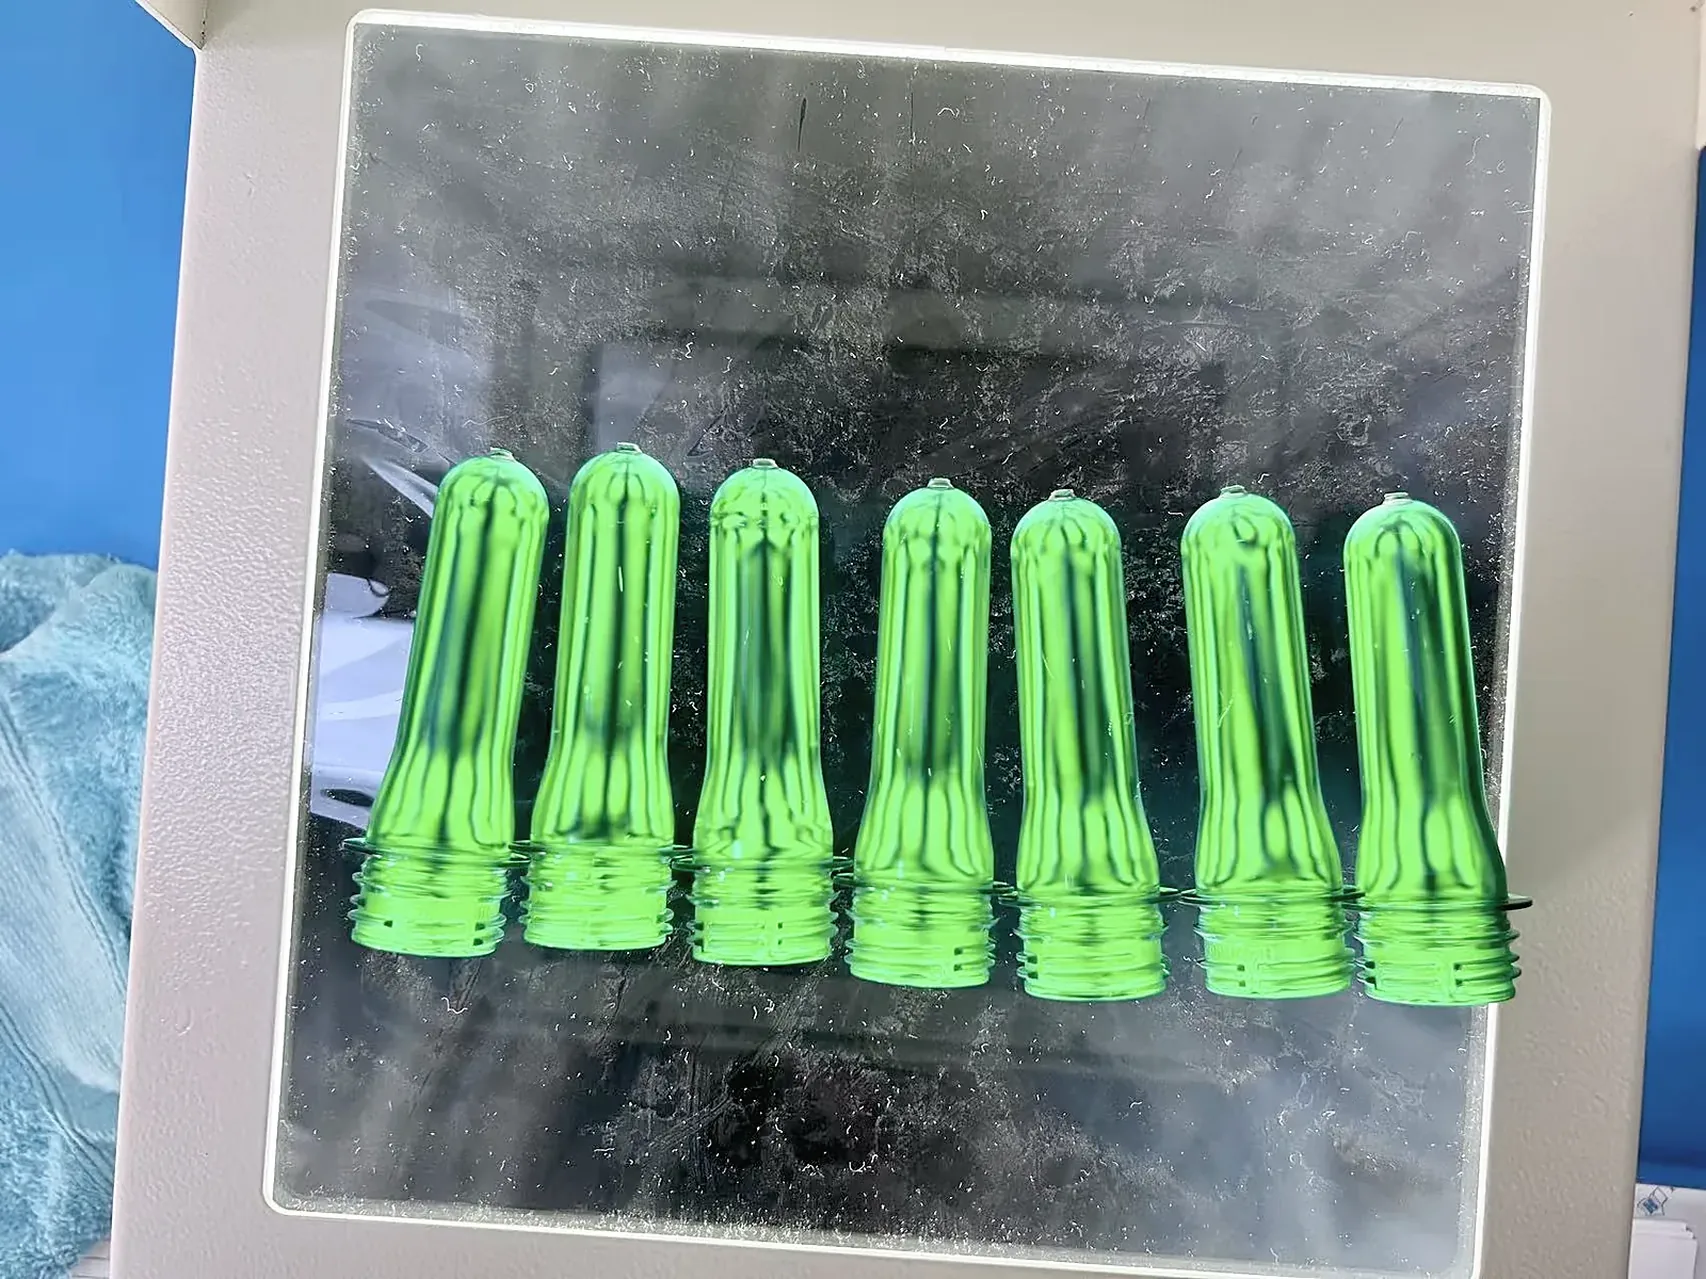
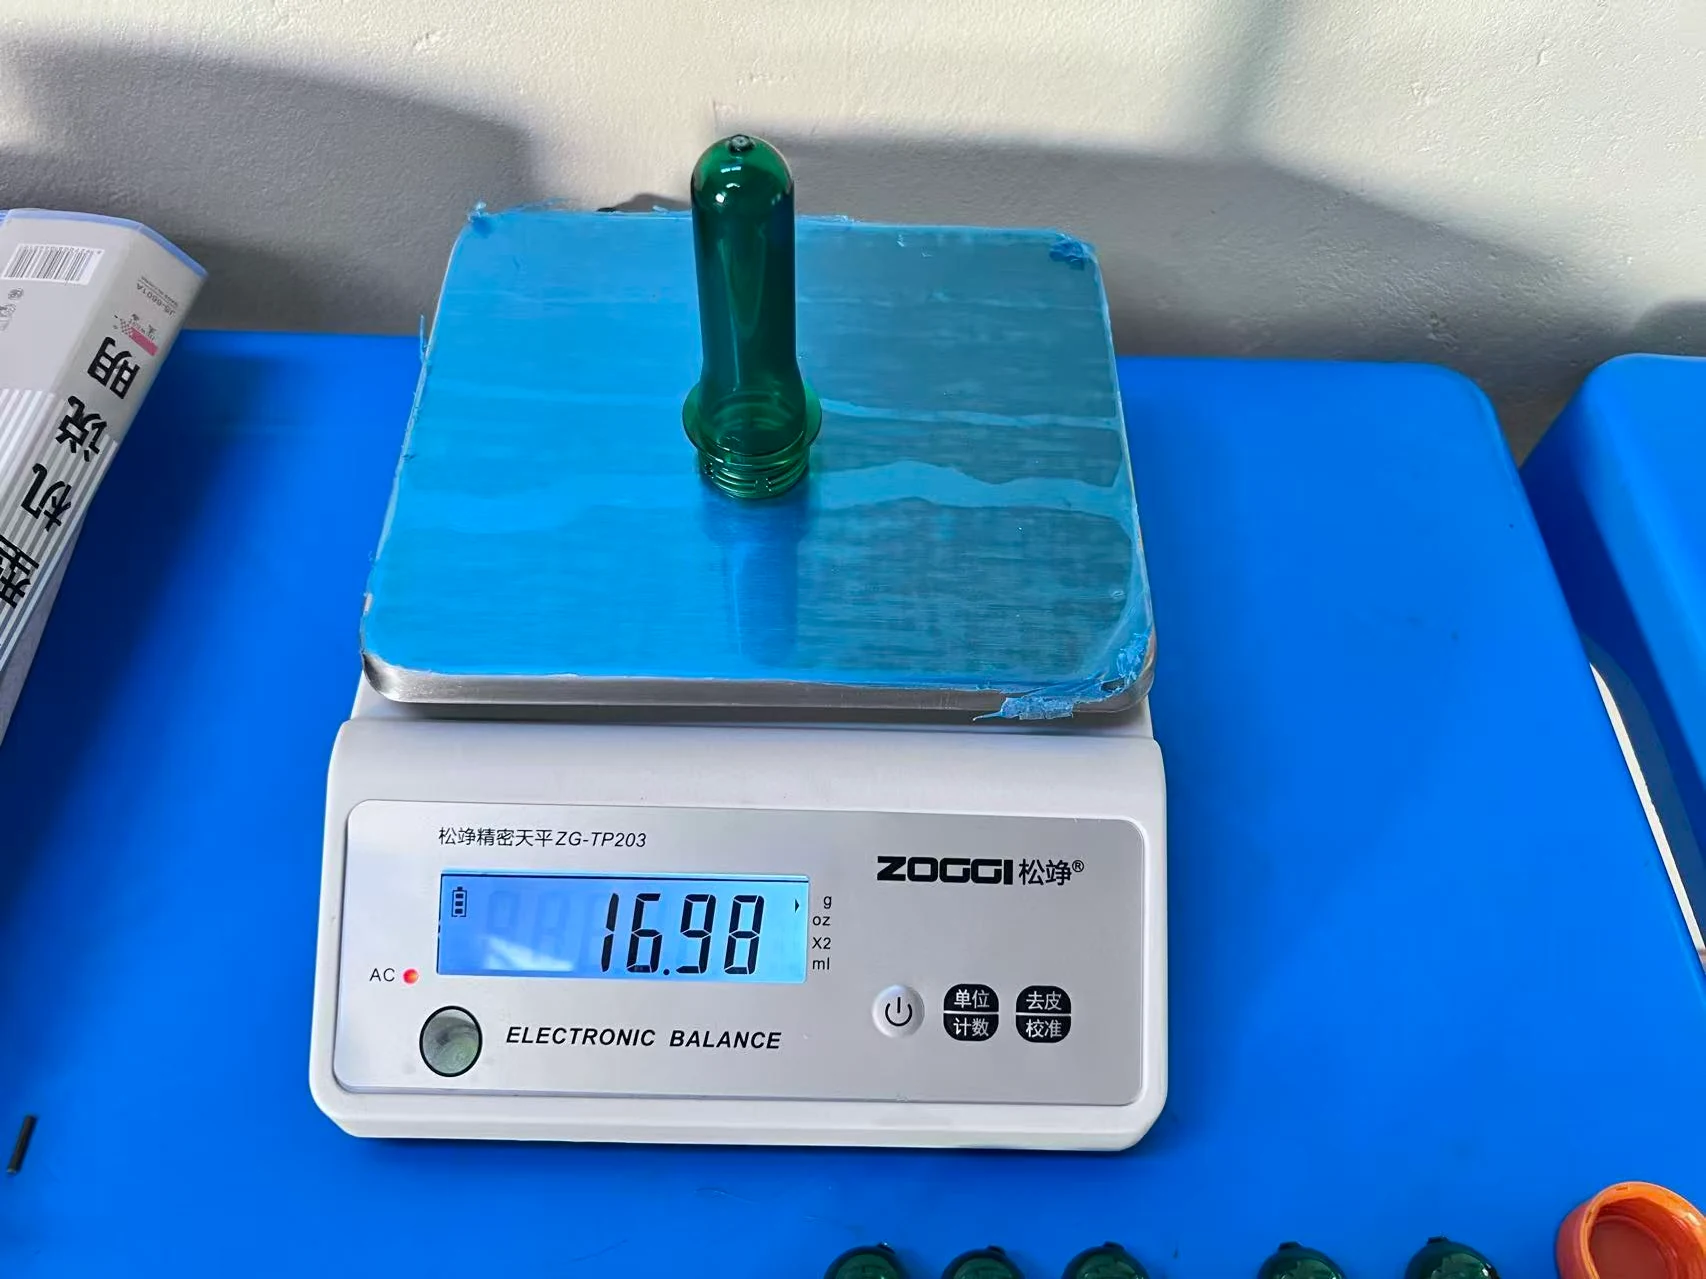
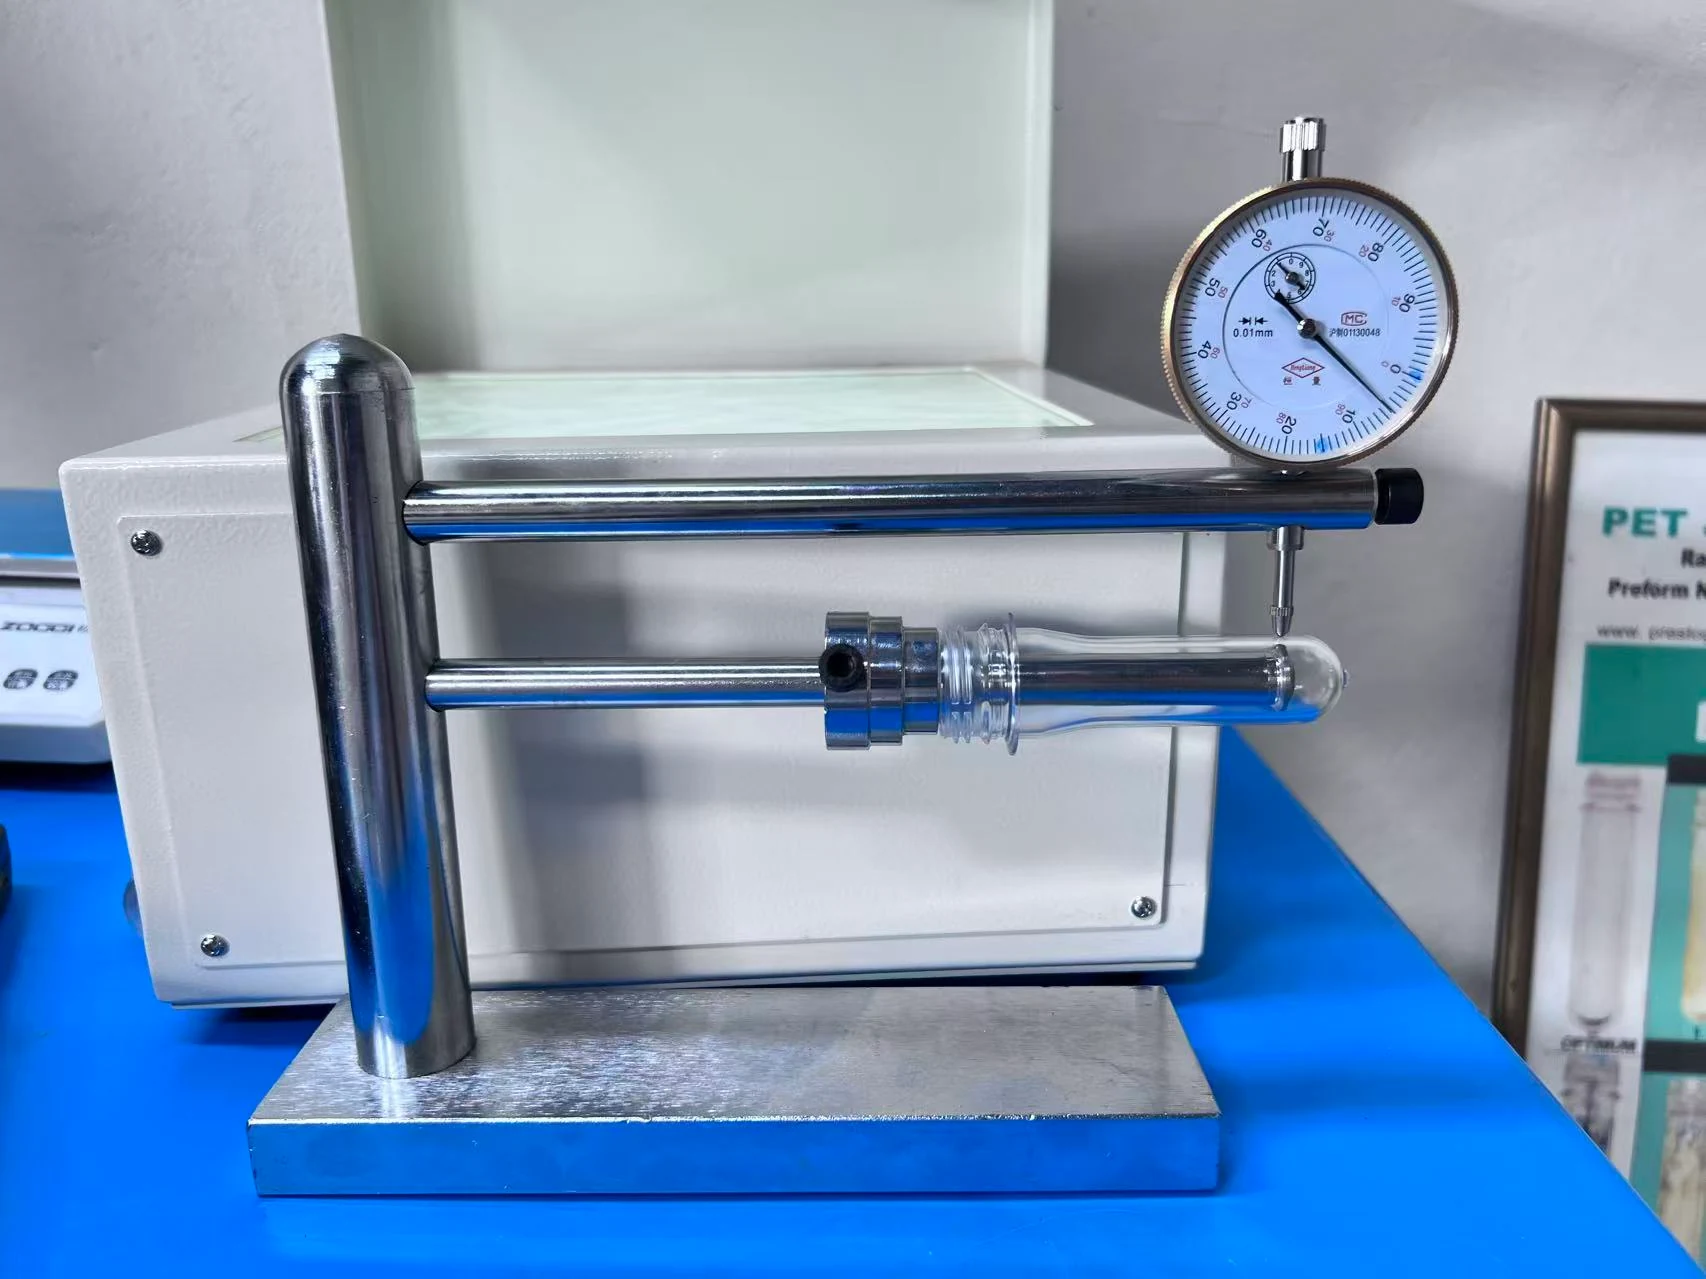
Use real manufacturing, assembly, inspection and trial evidence to evaluate the manufacturer behind the proposed configuration.
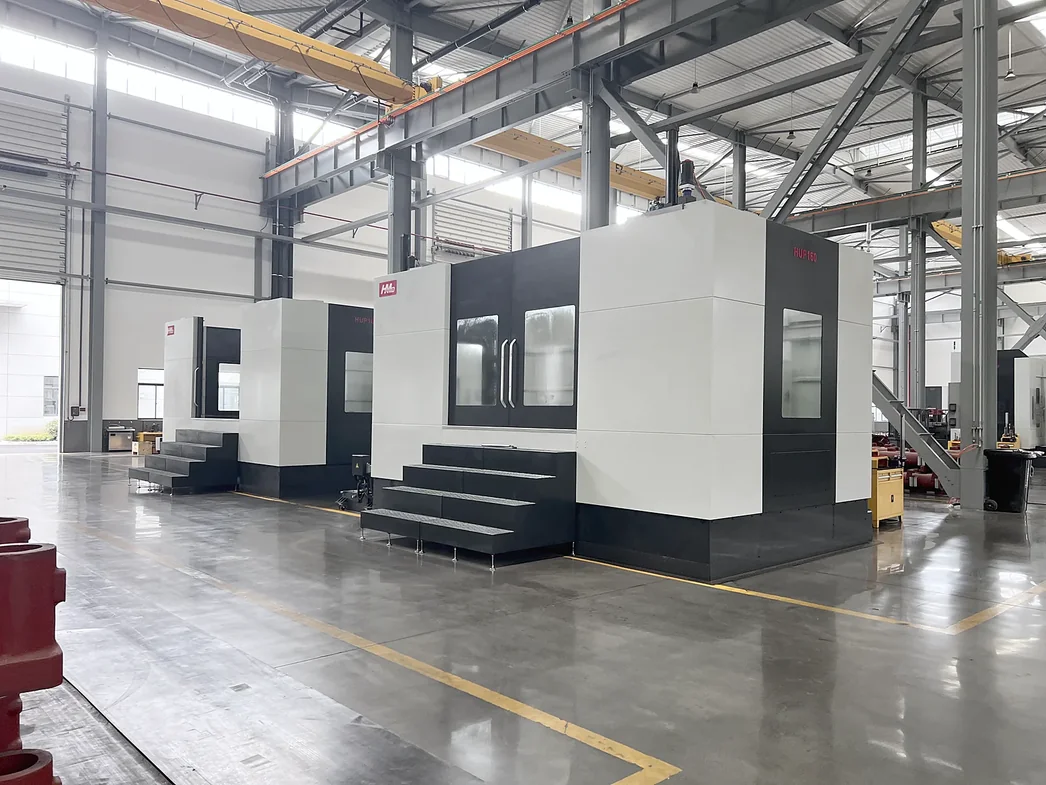
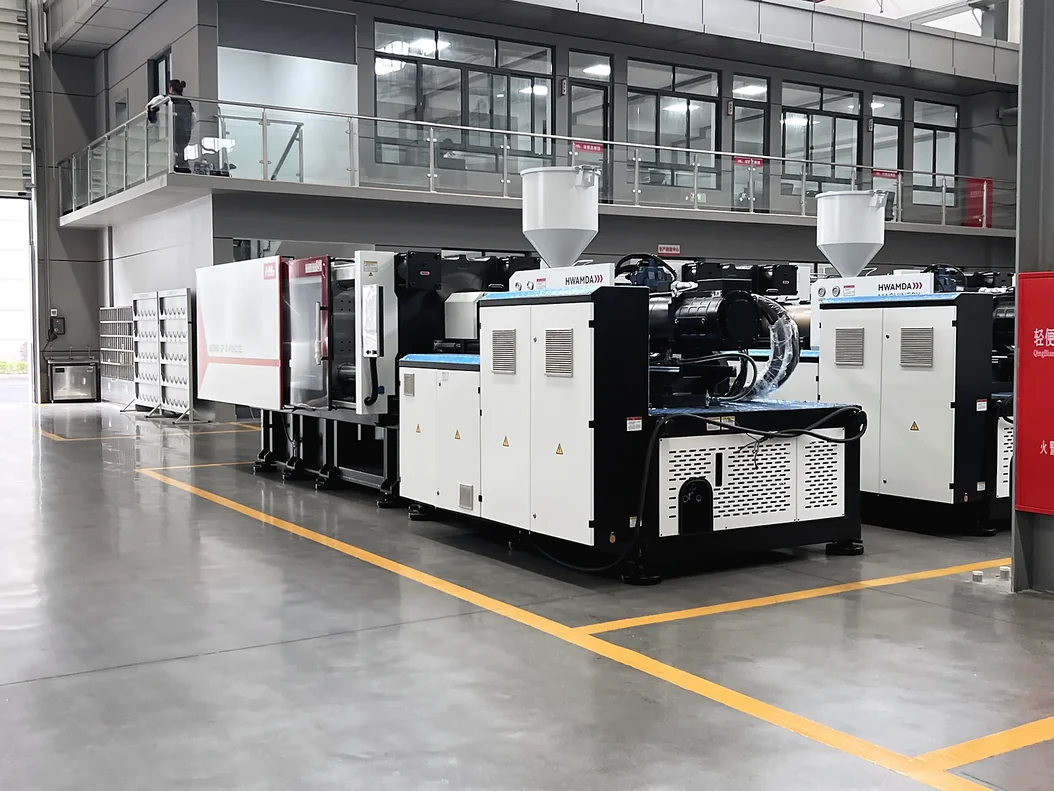
Use these answers to prepare the technical information needed for an accurate recommendation.
Multiply the preform weight by the cavity count to get the shot requirement, check it against the PET shot weight of each model, and check the mold against tie-bar spacing and mold thickness. In customer mold trials, the HMD320PET has run 48 × 15.2 g and 72 × 13 g molds, the HMD430PET 72 × 16.5 g and the HMD500PET 96 × 15.2 g. Send your preform and mold data for a model recommendation.
It depends on preform weight and mold size. The reference configurations show 32 cavities on the HMD268PET, up to 72 cavities on the HMD320PET and HMD430PET, and 96 cavities on the HMD500PET. Heavier preforms need more shot capacity per cavity: the HMD320PET runs 24 cavities of 85 g and 12 cavities of 135 g.
Send the preform weight and drawing, neck finish, mold cavity count or target output, resin, voltage and available plant utilities. Unknown values can be reviewed together.
Preform weight and wall thickness, cavity count, mold cooling, plasticizing recovery and take-out decide the stable cycle. Hourly output = cavities × 3,600 ÷ cycle time in seconds, before downtime and rejects. For example, 72 cavities at a 9.9 s cycle gives about 26,180 preforms per hour.
Price depends on the model and injection unit, cavity count and mold interface, auxiliaries, automation, utilities, logistics and service scope. Prices are quoted FOB Ningbo for each project. Auxiliary equipment, installation and training are optional and quoted per project, and the quotation lists every item included.
Yes, after checking mold dimensions, platen and tie-bar fit, injection requirement, ejector, hot runner, cooling and controls.
Yes. HWAMDA can include the PET preform mold in the project scope and verify the machine and mold together in a combined trial.
The final list depends on resin and output. Drying and dehumidifying, conveying, mold cooling, compressed air and take-out are normally reviewed. All auxiliary equipment is optional and quoted per project.
PET absorbs moisture from the air. Wet PET loses viscosity during melting, which affects preform clarity and strength, so the resin is dehumidified and dried to the resin supplier’s data before it reaches the screw.
Yes. HWAMDA can coordinate the machine with the mold, resin preparation, cooling, dosing, compressed air and take-out equipment according to the confirmed project scope.
Machine lead time is 60 working days. Mold, auxiliary equipment and shipping times are confirmed in the quotation for your project.
No. This machine injection-molds the preform. A separate blowing machine reheats and blows the preform into the final bottle.
Yes. HWAMDA supplies new PET preform machines for international projects, configured to the preform, mold, output target and plant utilities.
Send the basic project information first. Our sales engineer will help confirm the machine, mold and auxiliary-equipment details.