 HWAMDA
Bucket and lid geometry
Overall dimensions, nesting features, handle areas and demolding details affect the mold and handling review.

HMD M8SII SERIES
HMD M8SII configurations developed for 10–33 L paint bucket and lid production, with three-axis robot take-out or in-mold labeling. We match the machine, mold and automation to your bucket design.
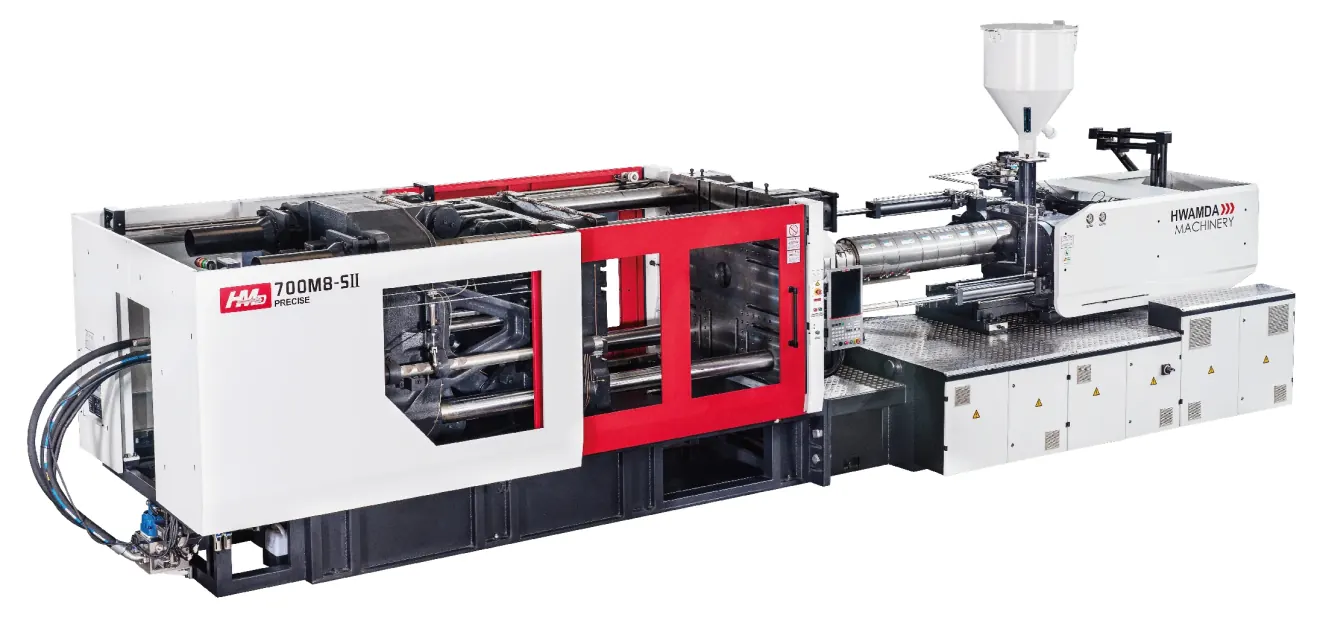
CAPACITY & HANDLING
Three-axis robot take-out and IML are offered as separate configuration groups, each with its own recommended bucket-capacity range. Choose the handling route first, then confirm the model with your bucket and mold data.
Recommended models for standard robot extraction after molding.
| Bucket capacity | Model | Clamping force | Injection weight | Mold thickness | Opening stroke | Tie-bar spacing | |
|---|---|---|---|---|---|---|---|
| 10L | HMD430M8-SII | 430 T | 1,646 g | 250–730 mm | 730 mm | 760×730 mm | Request review |
| 15L | HMD500M8-SII | 500 T | 1,858 g | 300–820 mm | 810 mm | 830×830 mm | Request review |
| 15–18L | HMD600M8-SII | 600 T | 2,324 g | 300–900 mm | 900 mm | 900×880 mm | Request review |
| 18–25L | HMD700M8-SII | 700 T | 2,903 g | 350–960 mm | 970 mm | 970×930 mm | Request review |
| 25–33L | HMD800M8-SII | 800 T | 3,225 g | 350–1000 mm | 1,040 mm | 1020×1000 mm | Request review |
Recommended models for in-mold labeled buckets.
| Bucket capacity | Model | Clamping force | Injection weight | Mold thickness | Opening stroke | Tie-bar spacing | |
|---|---|---|---|---|---|---|---|
| 10–15L | HMD500M8-SII | 500 T | 1,858 g | 300–820 mm | 810 mm | 830×830 mm | Request review |
| 15–18L | HMD600M8-SII | 600 T | 2,324 g | 300–900 mm | 900 mm | 900×880 mm | Request review |
| 18–22L | HMD700M8-SII | 700 T | 2,903 g | 350–960 mm | 970 mm | 970×930 mm | Request review |
| 25–33L | HMD800M8-SII | 800 T | 3,225 g | 350–1000 mm | 1,040 mm | 1020×1000 mm | Request review |
Capacity ranges are a starting point. The final model is confirmed with your bucket geometry, material, mold dimensions and output target.
PRODUCT REQUIREMENTS
Capacity alone does not determine a machine. Share the product and mold information you already have; unknown values can be confirmed during the project review.
Overall dimensions, nesting features, handle areas and demolding details affect the mold and handling review.
Provide the resin grade and actual molded weights. Shot weights in the tables use a PS reference, so the actual PP or HDPE bucket weight is needed for selection.
Confirm normal robot take-out, in-mold labeling or an undecided decoration route before defining the automation interface.
Share mold dimensions, cavities, runner concept and the required stable output or cycle target.
MODEL RANGE
Key machine and mold-interface values for the five paint bucket models. Use them for preliminary selection; the final configuration is confirmed in your quotation.
| Parameter | Unit | 430 | 500 | 600 | 700 | 800 |
|---|---|---|---|---|---|---|
| Injection volume(theoretical) | cm³ | 1,809 | 2,042 | 2,554 | 3,190 | 3,544 |
| Injection weight(PS) | g | 1,646 | 1,858 | 2,324 | 2,903 | 3,225 |
| Injection rate(PS) | g/s | 591 | 680 | 685 | 877 | 921 |
| Clamping force | kN | 4,300 | 5,000 | 6,000 | 7,000 | 8,000 |
| Mold opening stroke | mm | 730 | 810 | 900 | 970 | 1,040 |
| Dist. between tie bars (H×V) | mm | 760×730 | 830×830 | 900×880 | 970×930 | 1020×1000 |
| Mold thickness(Min–Max) | mm | 250–730 | 300–820 | 300–900 | 350–960 | 350–1000 |
| Machine dimension (L×W×H) | m | 8.0×2.0×2.6 | 8.3×2.1×2.6 | 9.9×2.3×2.5 | 10.4×2.4×2.7 | 11.5×2.5×3.3 |
Specifications: HWAMDA paint bucket machine catalog, July 2025 edition.
Complete injection, clamping, power and general specifications for each model.
| Parameter | Unit | 430 | 500 | 600 | 700 | 800 |
|---|---|---|---|---|---|---|
| Injection volume(theoretical) | cm³ | 1,809 | 2,042 | 2,554 | 3,190 | 3,544 |
| Injection weight(PS) | g | 1,646 | 1,858 | 2,324 | 2,903 | 3,225 |
| Injection weight(PS) | oz | 58.1 | 65.6 | 82 | 102.4 | 113.8 |
| Injection rate(PS) | g/s | 591 | 680 | 685 | 877 | 921 |
| Screw diameter | mm | 80 | 85 | 85 | 95 | 95 |
| Injection pressure | MPa | 158 | 155 | 174 | 166 | 181 |
| Screw L/D ratio | — | 22.5:1 | 22.8:1 | 23.3:1 | 24:1 | 23:1 |
| Screw stroke | mm | 360 | 360 | 450 | 450 | 500 |
| Screw speed | r/min | 0–173 | 0–165 | 0–160 | 0–180 | 0–181 |
| Parameter | Unit | 430 | 500 | 600 | 700 | 800 |
|---|---|---|---|---|---|---|
| Clamping force | kN | 4,300 | 5,000 | 6,000 | 7,000 | 8,000 |
| Mold opening stroke | mm | 730 | 810 | 900 | 970 | 1,040 |
| Platen size | mm | 1032×1042 | 1128×1168 | 1210×1250 | 1325×1345 | 1420×1440 |
| Dist. between tie bars (H×V) | mm | 760×730 | 830×830 | 900×880 | 970×930 | 1020×1000 |
| Max. daylight | mm | 1,460 | 1,630 | 1,800 | 1,930 | 2,040 |
| Mold thickness(Min–Max) | mm | 250–730 | 300–820 | 300–900 | 350–960 | 350–1000 |
| Ejector stroke | mm | 185 | 210 | 240 | 265 | 280 |
| Ejection tonnage | kN | 111 | 111 | 151 | 182 | 182 |
| Parameter | Unit | 430 | 500 | 600 | 700 | 800 |
|---|---|---|---|---|---|---|
| Hydraulic system pressure | MPa | 17.5 | 17.5 | 17.5 | 17.5 | 17.5 |
| Pump motor power | kW | 72 | 48+31 | 60+31 | 60+60 | 72+60 |
| Heater power | kW | 47.8 | 51.6 | 56.2 | 61.6 | 61.4 |
| Number of temp control zones | — | 6 | 6 | 6 | 6 | 7 |
| Parameter | Unit | 430 | 500 | 600 | 700 | 800 |
|---|---|---|---|---|---|---|
| Oil tank | L | 500 | 590 | 550 | 680 | 1,000 |
| Machine dimension (L×W×H) | m | 8.0×2.0×2.6 | 8.3×2.1×2.6 | 9.9×2.3×2.5 | 10.4×2.4×2.7 | 11.5×2.5×3.3 |
| Machine weight | Ton | 18 | 22 | 25 | 32 | 38 |
APPLICATION-SPECIFIC ENGINEERING
Four design features adapt the M8SII platform to deep bucket molds, heavy shots and fast handling.
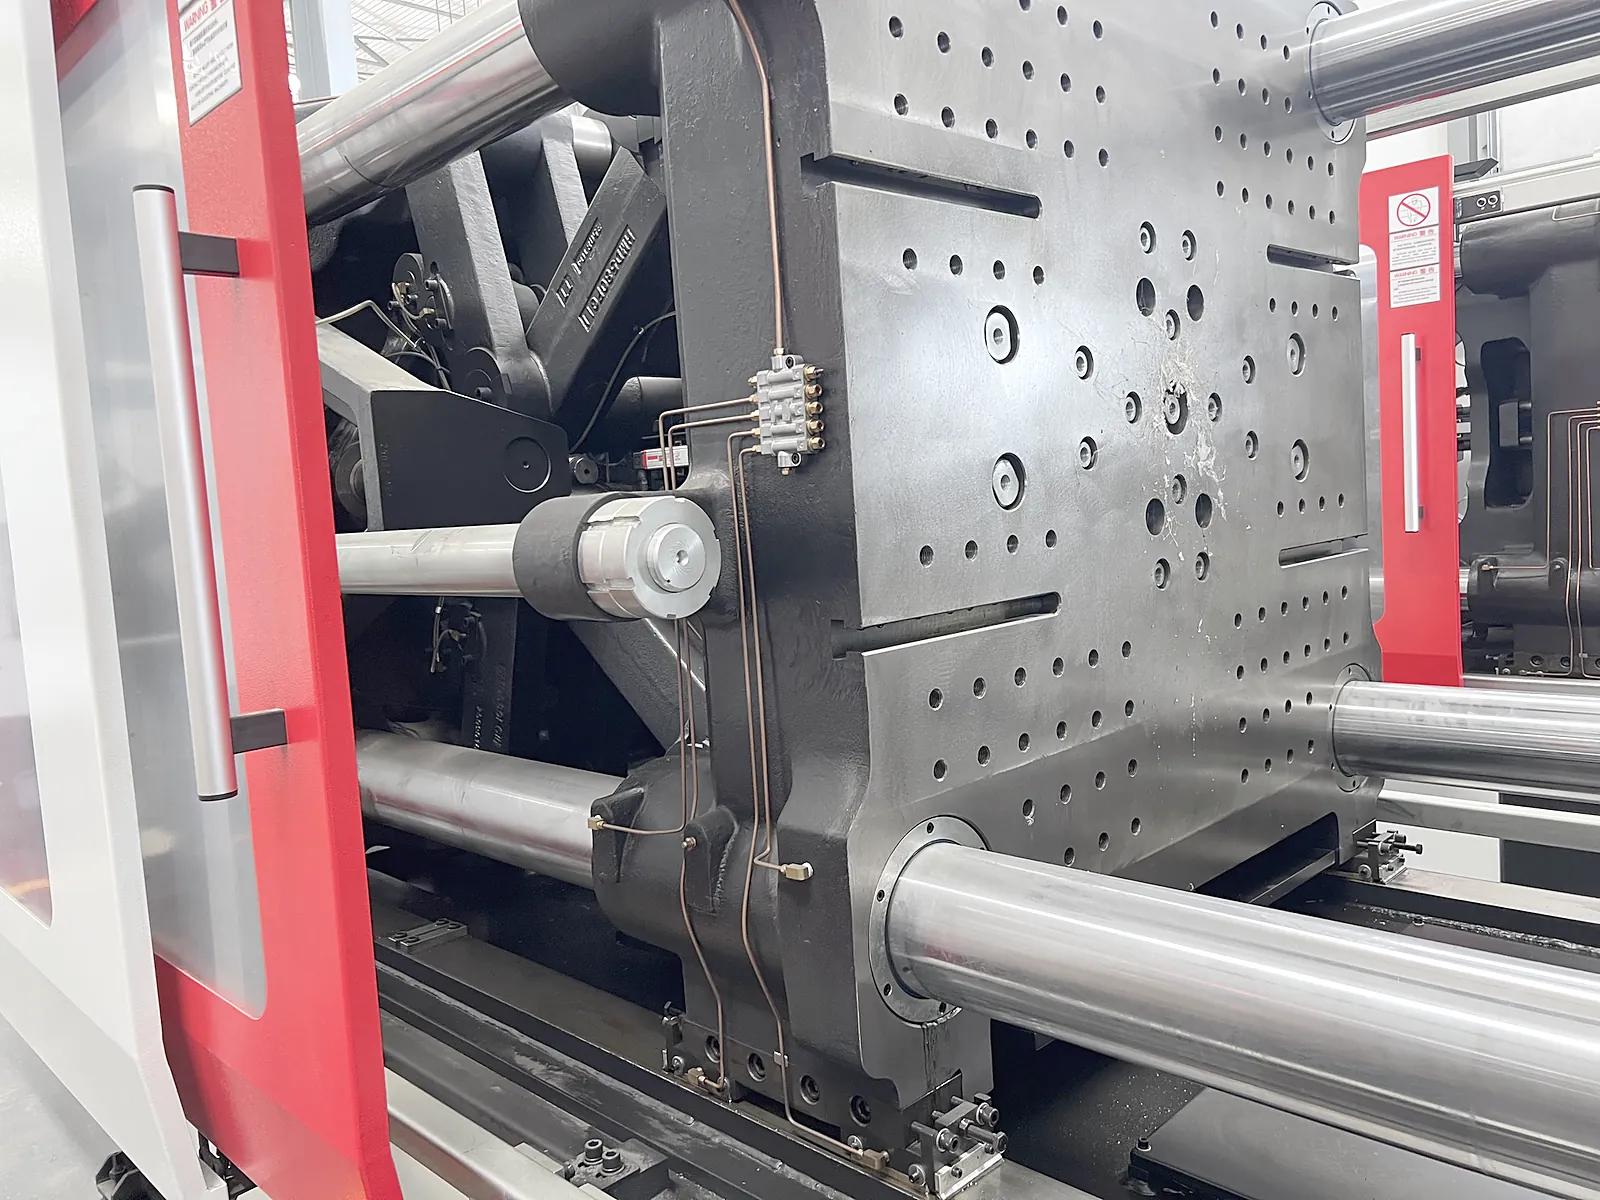
The platens are reinforced at the center, where deep bucket molds concentrate clamping load, to keep the mold supported and the parting line closed.
A bucket-specific screw and high-speed charging motor shorten plasticizing recovery for large PP and HDPE shots, so recovery keeps pace with the cycle.
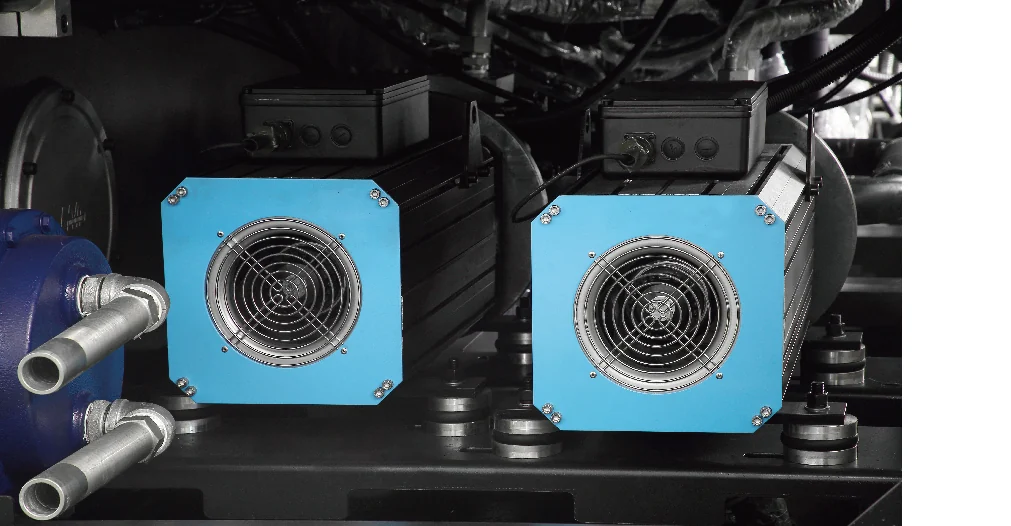
A dual-pump or enlarged servo system allows mold opening and ejection to run together, shortening the dry cycle on HMD500M8-SII and larger models.
Exception: HMD430M8-SII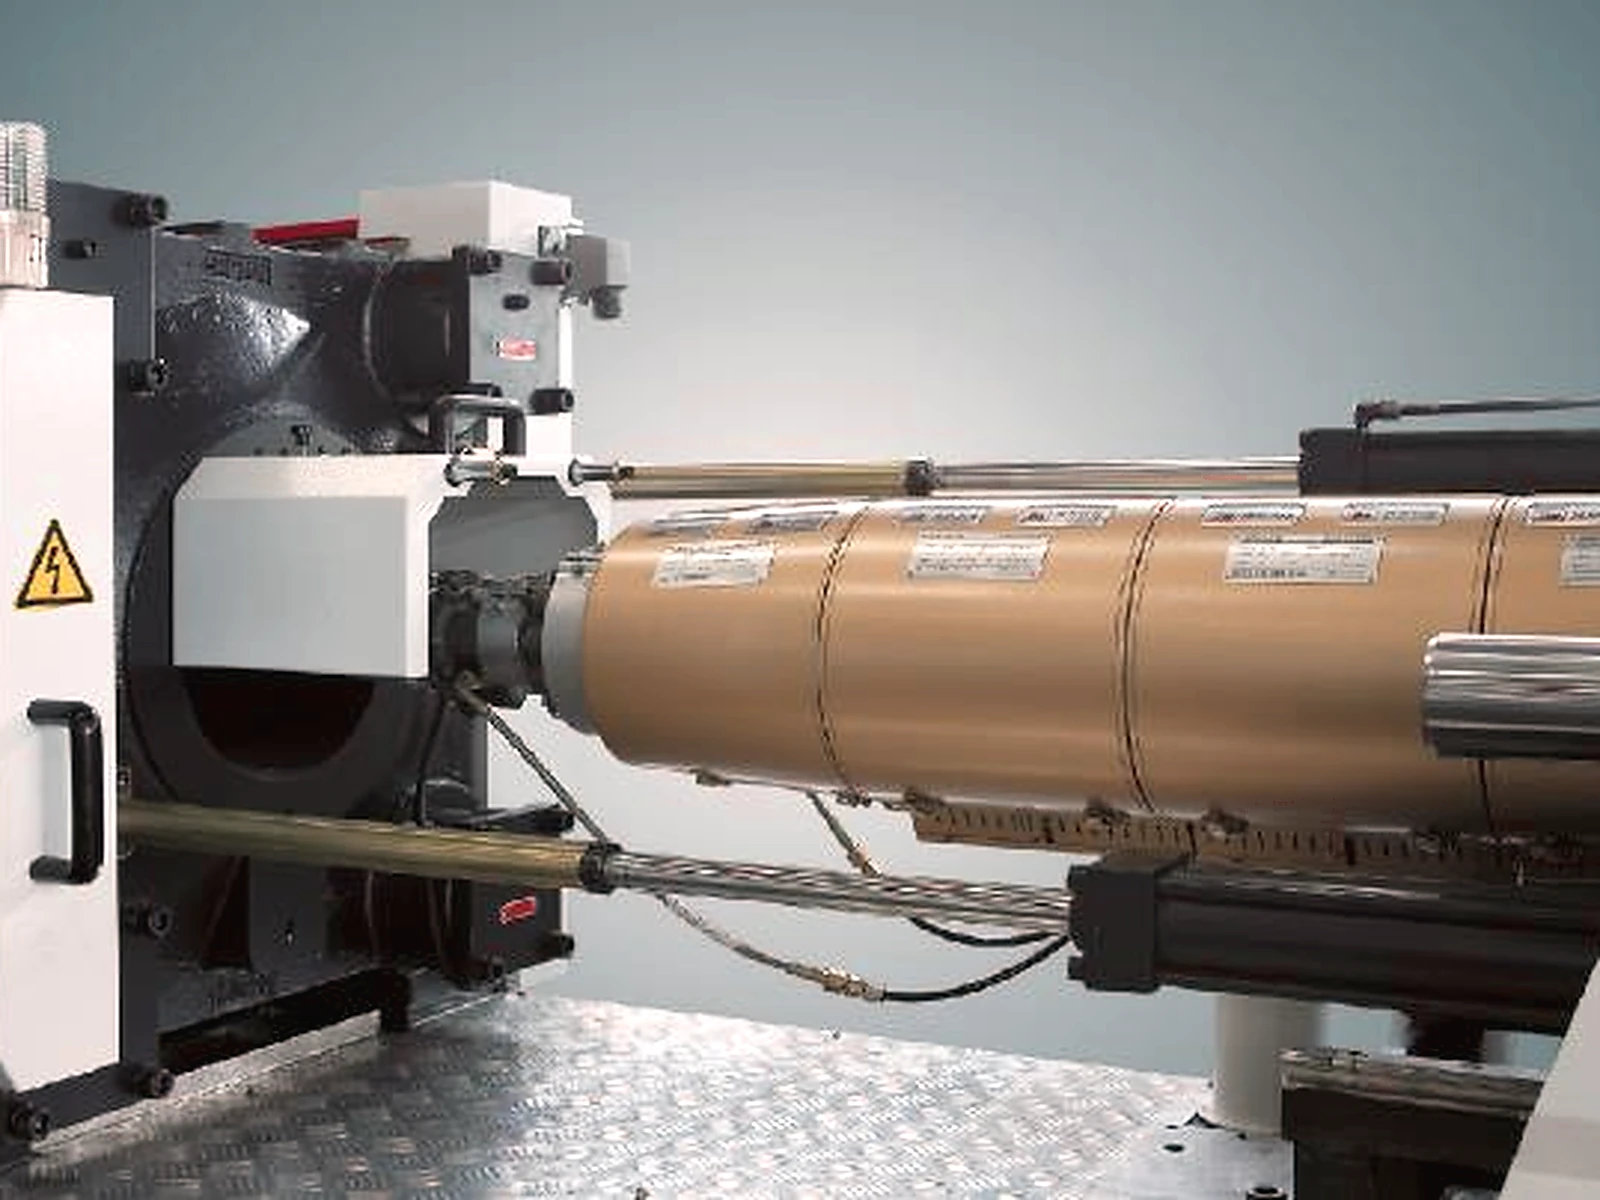
A 15+1 Φ12 quick-connect cooling-water manifold simplifies mold changes, and infrared barrel heating transfers heat directly to the barrel.
MACHINE–MOLD MATCHING
Bucket capacity is only a starting point. Machine fit is reviewed from the actual mold, runner, product and automation interfaces.
Confirm loading clearance, mounting footprint and connection positions.
Check installation, part release, robot access and safe demolding space.
Use the complete runner and cavity shot, resin basis and recovery requirement—not bucket volume alone.
Review ejector stroke and force, cooling circuits, robot signals and IML interface requirements.
Engineering review sequence
HANDLING, IML & PROJECT SCOPE
Choose a machine-only offer or a complete bucket production cell. Your quotation lists each item, from the mold and robot to IML and auxiliaries.
Machine configuration for the confirmed model
Robot interface and extraction requirement
Part release, placement and downstream handling
Machine and mold interface for IML
Label, robot and control requirements
Placement, inspection and stacking scope
Paint bucket and lid mold
Robot or IML equipment
Cooling and material handling
Installation, trial and acceptance boundary
CATALOG & TRIAL
The PDF catalog contains the full model tables, recommended bucket capacities and design features shown on this page.
Before shipment, the machine can be run with your bucket and lid mold, robot take-out or IML equipment under the trial and acceptance conditions agreed in your project.
PROJECT CONFIGURATION & PRICE
Send the bucket capacity, handling method and the product or mold information you already have. Missing engineering details will not block the enquiry.
Bucket and lid drawing or sample
Material and actual molded weight
Take-out, IML or not sure
Existing mold data and target output
BUYER QUESTIONS
With three-axis robot take-out, the five models cover buckets from 10 L up to 25–33 L. With IML, four models cover 10–15 L up to 25–33 L. The final model is confirmed from your bucket, mold and output target.
IML adds label placement and a different mold-opening and robot sequence. For example, HMD700M8-SII is recommended for 18–25 L buckets with standard take-out and 18–22 L buckets with IML.
HMD430M8-SII is offered as a standard take-out configuration. For IML buckets, HMD500M8-SII and larger models are the usual starting point; send your bucket and label details for a recommendation.
It is the shot weight calculated for polystyrene (PS), the industry reference material. For PP or HDPE buckets, the review uses your actual part weight and material.
It can be reviewed after checking mold dimensions, thickness, runner and shot requirement, platen and tie-bar fit, opening, ejector, cooling and automation interfaces.
Only the specific quotation defines what is included. Machine, mold, robot or IML equipment, auxiliaries, trial and service scope must be confirmed separately.
Cycle time depends on bucket size, wall thickness, material, mold cooling and the handling route. Send your bucket and mold data and we will estimate the cycle and confirm it in the machine trial.